Industrial Pump Repair Canada - Pump and Seal Repair and Replacement Services
ISO 9001 Certified
Industrial Pump Repair Canada - Pump and Seal Repair and Replacement Services
ISO 9001 Certified
Industrial equipment maintenance is entering 2026 under intense pressure. Factories must protect uptime while controlling labor, energy, and spare-parts costs. Reactive repairs remain expensive. Failures are expensive.
The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide reports that effective maintenance can reduce operating costs by approximately 5% to 20%. McKinsey research also indicates that predictive maintenance may cut machine downtime by 30% to 50% and reduce maintenance costs by 10% to 40%. These figures are encouraging, but they are not automatic results. Sensors are not magic.
A practical strategy begins with asset criticality. A vibration sensor on a motor can reveal bearing wear before abnormal noise reaches the production floor. Thermal imaging can identify a loose electrical connection during a scheduled inspection. A reliable CMMS can then connect that finding to a work order, technician, spare bearing, and documented repair history. ISO 55001 principles support this lifecycle approach by linking asset decisions with organizational objectives and measurable risk.
Yet data quality often remains weak. Technicians may record inconsistent readings. Alerts may arrive without clear thresholds. Some plants also invest in software before improving basic lubrication routines. That is a costly mistake worth reconsidering. The best industrial equipment maintenance programs combine preventive schedules, condition monitoring, operator experience, and disciplined safety procedures. This guide examines proven strategies, emerging technologies, and practical limitations for building a more resilient maintenance system in 2026.
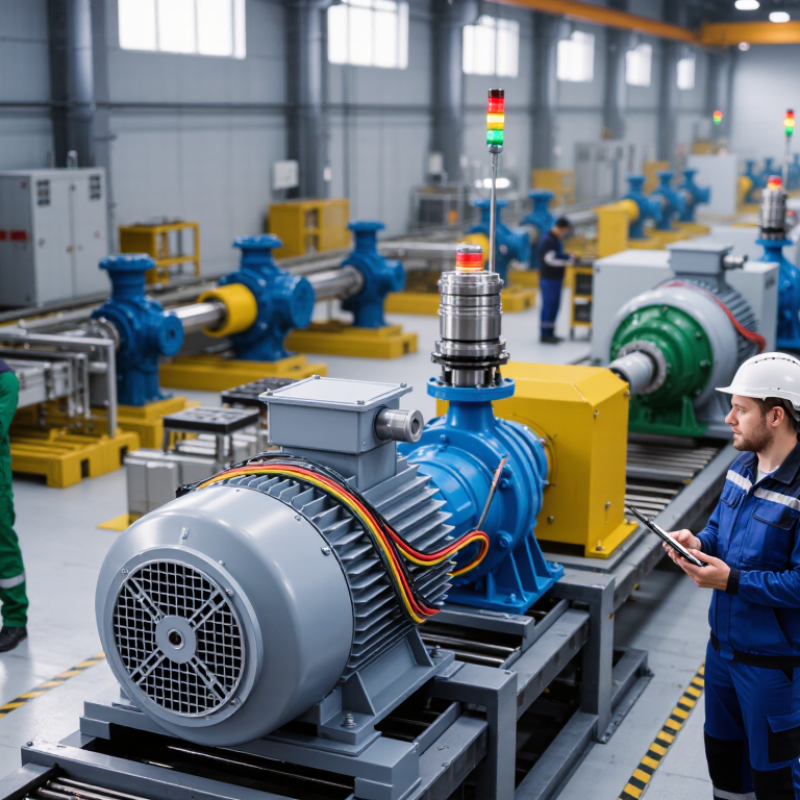
Industrial equipment maintenance is the planned care of machines, systems, and supporting assets. Its scope includes inspection, cleaning, lubrication, calibration, repairs, spare parts, documentation, and operator training. A technician may notice a hot bearing, a leaking seal, or unusual vibration before failure occurs. Small clues matter. Maintenance also protects energy performance, product quality, worker safety, and production continuity.
The U.S. Department of Energy’s Operations and Maintenance Best Practices Guide estimates that stronger maintenance practices can reduce energy consumption by 5% to 20%. That figure gives maintenance a wider purpose than fixing broken equipment. Core objectives include reducing unplanned downtime, extending asset life, controlling lifecycle cost, and improving predictable output. ISO 55001’s asset-management principles support this view by linking equipment decisions with organizational risk and performance. A practical program combines preventive schedules with condition-based checks. Use temperature readings, oil analysis, vibration trends, and failure histories. Not everything is predictable.
In my experience, the written schedule is rarely the complete truth. A pump may pass its monthly inspection but still fail after a process change. Teams should review work orders, alarm patterns, technician notes, and recurring delays together. Digital records help, but poor data creates false confidence. Operators need clear escalation rules, accessible manuals, and realistic maintenance windows. The aim is not to service every component more often. It is to perform the right work, at the right time, with evidence that supports the decision.
| Maintenance Area | Definition and Scope | Core Objective | Recommended Strategy for 2026 | Key Performance Indicators | Practical Reference or Target | Typical Review Frequency |
|---|---|---|---|---|---|---|
| Asset Register and Criticality | Identify equipment, components, locations, functions, failure consequences, and required maintenance resources. | Direct time and budget toward assets with the greatest safety, environmental, production, quality, or financial impact. | Maintain a standardized asset hierarchy and rank assets using consequence, likelihood, detectability, and regulatory importance. | Asset-register completeness; percentage of assets with criticality ratings; overdue criticality reviews. | 100% of production-critical assets identified; criticality method documented and consistently applied. | At commissioning and at least annually |
| Preventive Maintenance | Scheduled inspections, servicing, lubrication, calibration, adjustment, cleaning, and component replacement performed at planned intervals. | Reduce age-related failures and preserve equipment condition without creating unnecessary maintenance work. | Set task intervals from operating history, manufacturer instructions, failure patterns, safety requirements, and condition data rather than calendar habit alone. | Preventive-maintenance compliance; planned work percentage; repeat failures; maintenance-related downtime. | Use a documented tolerance window for scheduled tasks; investigate repeated failures instead of simply shortening intervals. | Weekly performance review; quarterly task optimization |
| Predictive and Condition-Based Maintenance | Maintenance decisions based on measured equipment condition, including vibration, temperature, lubricant condition, electrical characteristics, pressure, flow, or visual findings. | Detect developing faults early and perform intervention according to actual equipment health. | Combine sensor data with technician inspections and alarm thresholds; validate every alert with an actionable work order or documented disposition. | Alert-to-work-order conversion; confirmed-fault rate; warning time; avoided failures; false-alarm rate. | Apply monitoring first to high-criticality assets where early detection can change the maintenance decision. | Continuous monitoring or condition-based routes |
| Reliability-Centered Maintenance | A structured process that analyzes asset functions, functional failures, failure modes, consequences, and technically feasible tasks. | Select the most effective maintenance policy for each significant failure mode. | Use failure-mode analysis for critical systems and combine time-based, condition-based, failure-finding, run-to-failure, and redesign actions where appropriate. | Critical failure-mode coverage; functional-failure recurrence; risk reduction; maintenance-program changes implemented. | Prioritize systems whose failure consequences are severe and whose maintenance policy can materially reduce risk. | Initial study; review after major change or recurring failure |
| Planned Work and Scheduling | Preparation, parts reservation, labor assignment, permits, access planning, sequencing, and scheduling of maintenance work. | Increase wrench time, reduce delays, and make maintenance execution predictable. | Separate planning from scheduling, create job plans for recurring work, and coordinate maintenance windows with operations. | Schedule compliance; schedule break-in work; wrench time; planned work percentage; job-plan reuse. | Measure schedule compliance against an agreed weekly schedule and record reasons for variance. | Daily coordination; weekly scheduling meeting |
| Spare Parts and Materials | Identification, specification, procurement, storage, preservation, issuing, and replenishment of maintenance materials. | Prevent maintenance delays while controlling inventory cost, obsolescence, and stockout risk. | Classify parts by criticality and demand; link bills of materials to assets; verify shelf life and preservation requirements. | Stockout incidents; inventory accuracy; emergency purchases; obsolete inventory value; parts availability at job start. | Critical spares should have documented reorder logic, storage controls, and an owner responsible for periodic review. | Monthly inventory review; quarterly critical-spares review |
| Lubrication and Contamination Control | Selection, storage, identification, application, sampling, filtration, and cleanliness control for lubricants and hydraulic fluids. | Limit wear, overheating, corrosion, and premature component failure. | Use standardized lubricant identification, correct quantities, clean transfer equipment, and condition-based lubricant sampling for critical systems. | Lubrication-route compliance; lubricant-related failures; contamination findings; oil-analysis exceptions. | Define cleanliness and sampling limits for each application; never mix lubricants without compatibility verification. | Per route requirements; monthly trend review |
| Safety, Compliance, and Permit Control | Controls for hazardous energy, confined spaces, hot work, electrical hazards, working at height, chemicals, environmental obligations, and statutory inspections. | Protect personnel, the environment, and the operating license while ensuring maintenance is legally and procedurally controlled. | Integrate risk assessment, isolation verification, permit approval, competency checks, and closeout audits into every applicable work order. | Recordable incidents; permit deviations; overdue statutory inspections; isolation-verification findings; safety observations. | Zero overdue legally required inspections; all hazardous-energy work controlled by an approved isolation process. | Before each applicable task; formal audit at least annually |
| Failure Analysis and Continuous Improvement | Structured investigation of significant, repeated, or high-consequence failures using evidence from operating, maintenance, and inspection records. | Remove systemic causes rather than repeatedly restoring failed equipment. | Use root-cause analysis, evidence-based corrective actions, action owners, due dates, and effectiveness checks. | Repeat-failure rate; corrective-action closure; mean time between failures; verified effectiveness percentage. | Investigate failures according to consequence and recurrence, not only repair cost. | After significant failure; monthly action review |
| Digital Records and Data Quality | Collection and governance of asset data, work history, failure codes, measurements, labor, materials, and completion notes. | Create reliable information for planning, diagnosis, cost control, risk decisions, and lifecycle management. | Use controlled failure codes, mandatory completion fields, mobile data capture, approval workflows, and periodic data-quality checks. | Work-order closeout quality; missing-data rate; coding accuracy; percentage of records completed on time. | Every completed work order should record the asset, problem, cause, remedy, labor, parts, and functional status. | Daily validation; monthly data-quality audit |
| Lifecycle Cost and Renewal Planning | Evaluation of acquisition, operation, maintenance, energy, modification, downtime, disposal, and replacement costs over the asset life. | Optimize long-term value instead of minimizing only the immediate maintenance expense. | Use condition, risk, performance, obsolescence, energy use, and total-cost trends to support repair, refurbishment, redesign, or replacement decisions. | Maintenance cost per operating hour; downtime cost; energy intensity; renewal backlog; lifecycle-cost variance. | Review high-cost and high-risk assets using a documented lifecycle decision model. | Quarterly portfolio review; annual budget cycle |
In 2026, industrial maintenance planning begins with a clear equipment risk assessment. Experienced teams examine failure history, operating conditions, safety exposure, and production impact. A pump serving one production line may deserve more attention than five standby units. Context changes everything.
Criticality ranking should combine likelihood and consequence. Reviewers can score safety, environmental impact, downtime, repair cost, and spare-part availability. Use site evidence, not assumptions. Small clues matter. A rising bearing temperature, repeated alarm, or delayed lubrication can reveal a developing failure. Inspections should also consider equipment age, workload, installation quality, and operator reports.
Maintenance requirements must match the risk. Critical rotating equipment may need vibration checks, oil analysis, thermal inspections, and planned overhauls. Lower-risk assets may only require scheduled checks and corrective work. Digital records can expose recurring failures, but poor data creates false confidence. Keep the method simple enough for technicians to use consistently.
No assessment is perfect. Early reviews often overrate familiar machines and overlook support systems, such as cooling or compressed air. Reassess rankings after modifications, incidents, process changes, or repeated defects. One practical improvement is comparing planned tasks with actual failure patterns each quarter. That comparison may expose unnecessary inspections, missing controls, or maintenance intervals that no longer fit the equipment.
Industrial equipment maintenance in 2026 should begin with risk, not technology. A preventive plan schedules inspections, lubrication, alignment, and component replacement according to operating hours. It protects predictable assets, such as conveyor bearings and hydraulic filters. However, calendar-based work can replace healthy parts too early.
Condition-based maintenance adds evidence. Technicians can inspect vibration, temperature, oil particles, pressure, and electrical current. Set practical alarm limits for each machine. A hot bearing housing or rising vibration trend deserves attention before failure. The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide reports that predictive maintenance can reduce costs by 8–12% compared with preventive maintenance, and by 30–40% compared with reactive work.
Predictive maintenance needs disciplined data. McKinsey’s analysis, “Predictive Maintenance: The Next Frontier,” estimates potential maintenance-cost reductions of 10–40% and downtime reductions of 30–50%. These figures are promising, but they are not automatic results. Poor sensor placement creates false alarms. Incomplete failure histories weaken models. Keep humans involved. Experienced technicians should validate alerts against noise, load, weather, and recent repairs. Start with critical assets and clear failure modes. A simple inspection route may outperform an expensive system when data quality is weak. The plan should also record response time, avoided failures, spare-part use, and repeat defects. It will not be perfect. Monthly reviews can expose blind spots and adjust thresholds before small errors become costly stoppages.
2026 Best Industrial Equipment Maintenance Strategies
In 2026, maintenance teams will connect digital tools with practical human judgment. Start with failure modes. The U.S. Department of Energy’s Operations and Maintenance Best Practices Guide reports that predictive maintenance can reduce maintenance costs by 30–40% and downtime by 35–45%. These gains require clean sensor data, consistent inspections, and alarms linked to work orders. A vibration trend should trigger a bearing check, not merely another dashboard notification.
Workforce capability matters just as much. The World Economic Forum’s 2023 Future of Jobs Report estimates that 44% of workers’ core skills will change within five years. Technicians therefore need training in vibration analysis, basic data interpretation, electrical safety, and root-cause analysis. Keep lessons near the machine. A five-minute demonstration beside a noisy motor may teach more than an hour-long presentation. Digital tools cannot replace judgment.
Workflows must remain simple. Define clear escalation rules, spare-parts ownership, and approval limits before equipment fails. Review completed work orders weekly. Look for repeated temporary repairs. They are warning signs. Some plants overinvest in sensors while ignoring lubrication discipline and overdue inspections. That is an expensive mistake. A useful pilot might monitor one compressor, compare predicted failures with actual findings, and adjust thresholds monthly. The process will not be perfect. It should become more reliable through measured correction.
Benchmark targets for digital maintenance workflows, workforce capability, and execution discipline.
The benchmark targets emphasize moving work from reactive response to planned execution: at least 80% planned work, 90% schedule compliance, 90% preventive-maintenance compliance, and approximately 55% technician wrench time. Digital work-order tools, condition monitoring, standardized workflows, and continuous skills development support these outcomes.
Effective industrial maintenance begins with measurable performance, not assumptions. In field operations, I track planned maintenance compliance, mean time between failures, and mean time to repair. These figures reveal whether teams prevent failures or merely react to them. A weekly review should connect work orders with machine downtime, spare-part delays, and technician hours. Simple data often exposes expensive habits.
Safety outcomes require more than counting injuries. Teams should monitor near-miss reports, overdue inspections, lockout verification, and repeated access hazards. A maintenance area may appear orderly while isolation steps remain inconsistent. Short interviews with technicians can uncover risks that dashboards miss. Record the condition of guards, platforms, tools, and floor surfaces during routine inspections. Evidence matters.
Continuous improvement works best through small, tested changes. After a recurring pump failure, compare lubrication records, vibration readings, alignment checks, and operating conditions. Change one factor, then measure the result. Not every improvement succeeds. We once treated delayed repairs as a staffing problem, but poor fault descriptions caused much of the delay. That mistake changed our training focus. Managers should publish actions, owners, deadlines, and verification results. If a metric improves while near-miss reporting falls sharply, question the data before celebrating.